Elevate Bottle
In an era defined by unpredictable environmental shifts and a surging interest in "off-grid" living, the Survival Water Bottle industry has evolved from a niche tactical market into a multi-billion dollar global powerhouse. No longer restricted to military personnel, today's survival water bottles are essential gear for outdoor enthusiasts, disaster relief organizations, and urban preppers alike.
As a leading Survival Water Bottles Factory & Exporter, we recognize that the demand is shifting towards multi-functional products. Global procurement trends show a massive uptick in the need for bottles that offer not just storage, but active filtration, extreme temperature resistance, and unparalleled durability. North American and European markets are leading this demand, with a specific focus on BPA-free materials and sustainable manufacturing processes.
The industrial status of this sector is currently characterized by high-precision engineering. Factories are now integrating medical-grade stainless steel (316L), aerospace-grade titanium, and advanced polymers to ensure that these vessels can withstand the harshest conditions on Earth—from the scorching Sahara to the freezing Arctic.
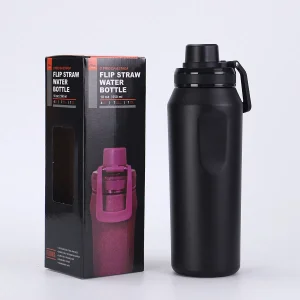
Modern survival gear now includes UV-C purification caps and hydration tracking sensors, ensuring water safety through AI-driven diagnostics.
The shift towards eco-friendly materials is paramount. Reusable, long-life bottles are replacing single-use plastics in global relief efforts.
Interoperability with MOLLE systems and standard filtration threads (like Sawyer or LifeStraw) is now a standard requirement for exporters.
We are witnessing a revolution where weight-to-strength ratios are being optimized. Our factory utilizes double-wall vacuum insulation technology that can keep water ice-cold for 48 hours in a desert environment. This isn't just about comfort; in a survival situation, maintaining body temperature and having access to cool water is a critical safety factor. Furthermore, the integration of Hollow Fiber Membrane filtration systems directly into the bottle structure is the next frontier we are currently developing in our R&D labs.
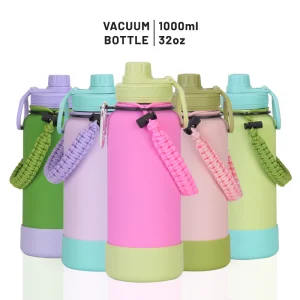
This premium 1L double-wall stainless steel vacuum bottle represents the pinnacle of survival gear. Designed for extreme sports and tactical operations, it features a wide-mouth design for easy cleaning and compatibility with standard water filters. The powder-coated finish ensures a non-slip grip even in wet conditions.
In the global B2B marketplace, procurement officers from NGOs, military contractors, and retail giants look for more than just a bottle; they look for a reliable supply chain partner. The key demands in 2024-2025 include:
China remains the undisputed leader in survival water bottle manufacturing due to its complete industrial ecosystem. At Zhejiang Elevate Bottle Co., Ltd., we leverage local access to high-grade raw materials and advanced robotic automation, allowing us to offer prices that are 30-40% more competitive than Western alternatives without sacrificing a single degree of quality.
During floods or earthquakes, portable water storage is the difference between life and death. Our lightweight PET and glass options are used by NGOs for rapid deployment.
Soldiers require hydration that won't fail in the field. Our stainless steel vacuum series is built to military specifications for noise reduction and durability.
From mountaineering to long-distance trekking, our bottles provide the reliable hydration needed for the most strenuous human endeavors.
This high-tech 304 stainless steel vacuum bottle is equipped with an LED temperature display, perfect for business gifts or extreme environment monitoring. It represents our factory's commitment to merging traditional survival gear with modern AI-driven technology.
Zhejiang Elevate Bottle Co., Ltd. is a professional enterprise with designing, developing, manufaturering and marketing of stainless steel vacuum flasks, borosilicate glass bottles , plastic water bottles and titanium cups. They are 100% food-safe grade, comply with European and American food safety standards. We have rich experience in OEM and ODM services, and our R&D team is able to form more than 20 pieces of new product design solutions every year. Meanwhile, our factory has invested in several automated production lines, which are done automatically by robots, which greatly reduces production time and labor costs. With our outstanding R&D and design capabilities, good product quality and cost performance, and fast product delivery, we have helped many startups grow together and help them profit from their projects. If you are interested in any of our products or would like to discuss a custom order, please do not hesitate to contact us. Our sales will work fully for you!
Strong foundation, flexible water bottle design experience
To deliver end-to-end solutions, we leverage our expertise in design, engineering, manufacturing, and logistics. Elevate Bottle capabilities span from concept creation and industrial design to mold fabrication, production, warehousing, and global distribution, driving rapid growth for your brand and business.
Annually, Elevate Bottle launches over 120 competitive new products. Our diverse product line spans multiple materials and use cases, meeting a wide range of customer needs.
The R&D team has developed and patented smart chip technologies and proprietary components for smart water bottles, offering features like temperature display and control, hydration tracking, and health monitoring. Additionally, the app provides sleek, digital functions meeting evolving market demands.
As we look towards the next decade, the role of a survival water bottle factory will change from a simple manufacturer to a technology partner. The integration of AI and IoT into hydration products is no longer a futuristic dream. Smart bottles that can alert a user to drink more water or test the quality of the water inside are currently in production. This level of innovation is driven by the global need for smarter survival tools that provide data-driven health benefits.
For international buyers, the challenge is finding a factory that can balance this technological innovation with the raw ruggedness required for survival gear. At Zhejiang Elevate Bottle Co., Ltd., we meet this challenge by maintaining a rigorous quality control system. Each bottle undergoes a series of stress tests, including drop tests from 5 meters, vacuum retention tests for 24 hours, and leak-proof cycle tests. Our commitment to zero-defect manufacturing is why we remain a top choice for exporters worldwide.
In addition to performance, we are deeply committed to environmental stewardship. The survival industry is inherently linked to the appreciation of nature. Therefore, we have invested in eco-friendly coating processes and 100% recyclable packaging solutions. We believe that protecting the planet is just as important as protecting the person using our bottles in the wilderness.
Whether you are a startup brand looking to enter the tactical gear market or an established wholesaler searching for a more reliable OEM partner in China, we invite you to experience the difference that advanced engineering and ethical manufacturing can make. Our 10,000+ square meter facility is equipped with the latest robotic arms and precision molding machines to bring your vision to life. Contact our sales team today to discuss your custom project and join our network of global success stories.